CO+ sensor
Monitor combustion. Guide optimization. Improve efficiency.
What the CO⁺ Sensor does.
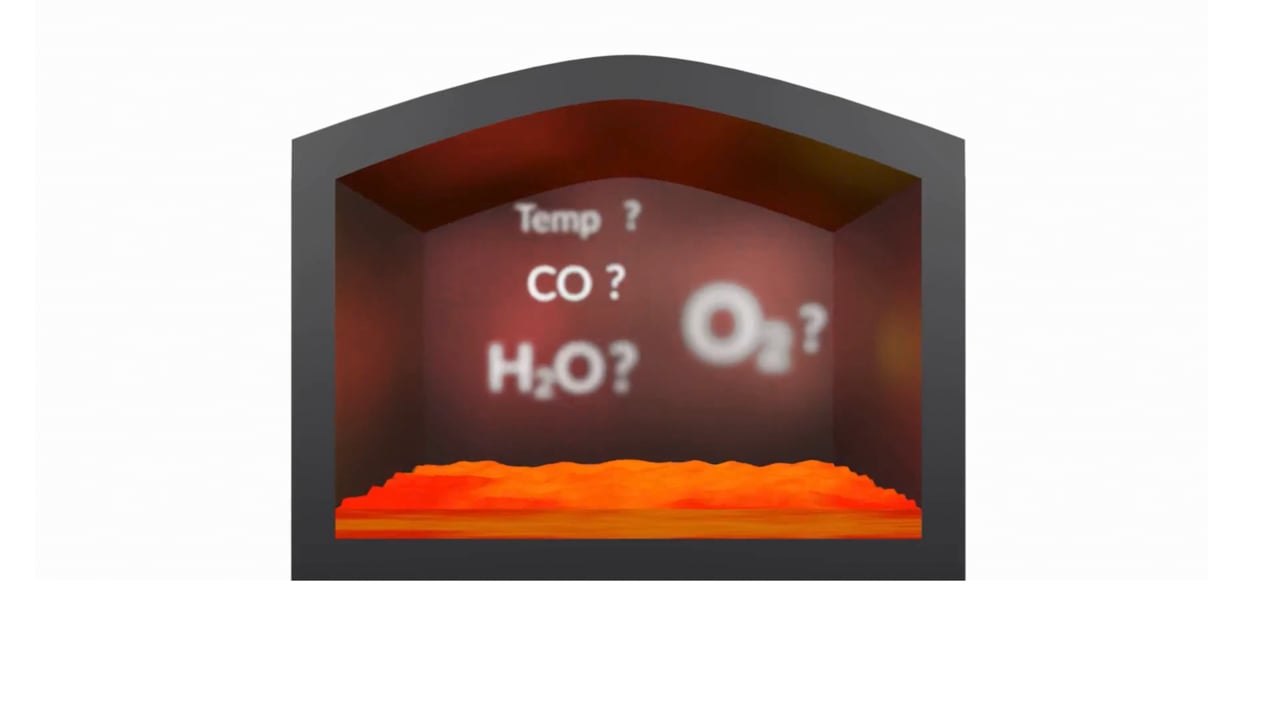
The CelSian CO+ Sensor is the first non-invasive combustion monitoring solution developed specifically for the glass industry. The CO⁺ Sensor continuously measures and monitors CO, O₂, temperature and humidity levels in flue gases, allowing operators to fine-tune the combustion with precision. This real-time insight transforms combustion control from guesswork into data-driven action. The CO⁺ Sensor helps glass manufacturers achieve higher energy efficiency, more stable combustion, and lower emissions.
Laser-specific advantages
- Non-contact method, no degradation issues, long lifetime (>10 years for laser).
- Continuous recording of digital signals, enabling data processing and quick process analysis (correlations to O₂/gas ratio, fuel use, flue gas emissions, etc.).
- Measuring over the full width of the flue gas channel providing representative values.
- No drift, self-correcting for varying laser beam transmission (so no manual checks needed).
- Alarm function in case of sensor malfunctioning (e.g. laser beam blockage).
How the CO⁺ sensor Helps
through optimized and stable combustion.
typically around 2% for end-port furnaces
to melt by more luminous flames
in oxy fired furnaces (typically 1000 m³ O₂/day for a 250 ton/day furnace)
like post-combustion and higher sodium and SO₂ evaporations
CO⁺sensor in Action
Excess oxygen and unstable combustion were driving up both emissions and cost in a container glass furnace.
Installing the CO⁺ Sensor allowed operators to precisely monitor CO and/or CO₂ levels, leading to real-time tuning of combustion settings.
Impact:
- 20% reduction in NOₓ emissions
- 1,000 m³/day oxygen savings
- Improved energy efficiency
It is difficult to maintain a consistent combustion balance when relying entirely on manual air and gas adjustments.
Integrating the CO⁺ Sensor into the container glass furnace's control system, the process shifted to fully automatic regulation based on real-time flue gas feedback.
Impact:
- 3% reduction in overall energy consumption
- Stable operation and improved temperature control
An insulation wool producer was facing high oxygen consumption and reduced combustion efficiency. Installation of the CO⁺ Sensor revealed flue gas oxygen levels of 8%, enabling operators to optimize combustion and achieve measurable improvements within three months.
Impact:
- 50% reduction in excess oxygen (from 8% → 4%)
- Significant fuel and oxygen savings
- Stable, efficient combustion
Proven concept
- For a ~280 ton/day oxy fuel container furnace.
- NOx emissions drop with 20%.
- O₂ savings 1000 m³/day.
- Gas savings of 1 – 2% (~525 m³/day).
- Return on investment < 1 year.

Trusted by More Than 60 Glass Plants Worldwide
The CelSian CO+ Sensor has been successfully installed in more than 60 sites. Most applications are in end-port furnaces and oxy-fired furnaces (Soda lime and E-glass), where the CO+ Sensor has become the standard type of measurement for measuring CO and oxygen as part of the rebuild specification, helping reduce energy costs and improve product quality.
Installation is easy and can be done both on new and running furnaces.